PCB press-fit connector assembly
Servo press evaluation for compliant pins, SFP cages and backplane connectors.
PCB connector press-fit guide
Servo press-fit systems, tooling, and integrated stations for electronics, motor, and automotive production lines. Validate the joint with samples before specifying cycle time and acceptance.
Start with your part, joining risks, and inspection requirements to assess equipment and tooling fit.
Servo press evaluation for compliant pins, SFP cages and backplane connectors.
PCB connector press-fit guidePart and tooling evaluation for motor shafts, bearings and end caps.
Motor and bearing press-fit guideInterference-fit assembly and validation for suspension bushings, subframe supports and hub components.
Automotive bushing press-fit guideSpecify force, usable stroke, fixture clearance, and part loading for the station.
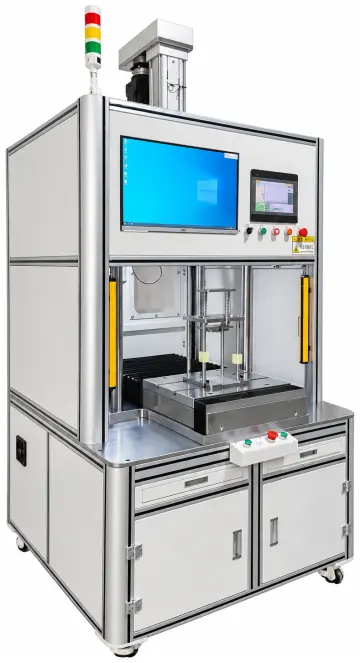
For bearings, bushings, shafts and motor components. Compare C-frame and four-column configurations, then confirm the force–displacement criteria with samples.
Servo press selection and specifications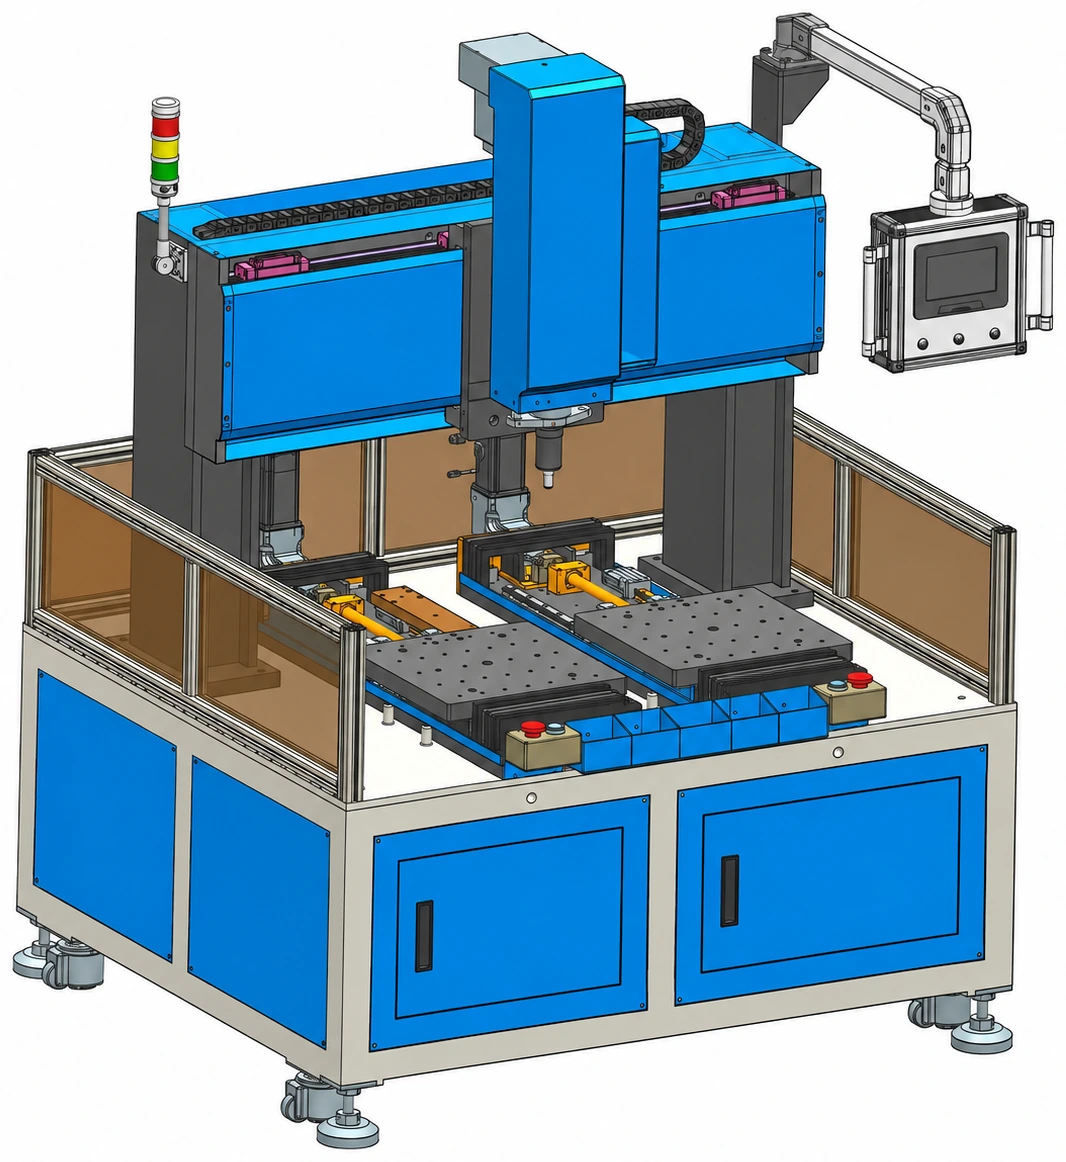
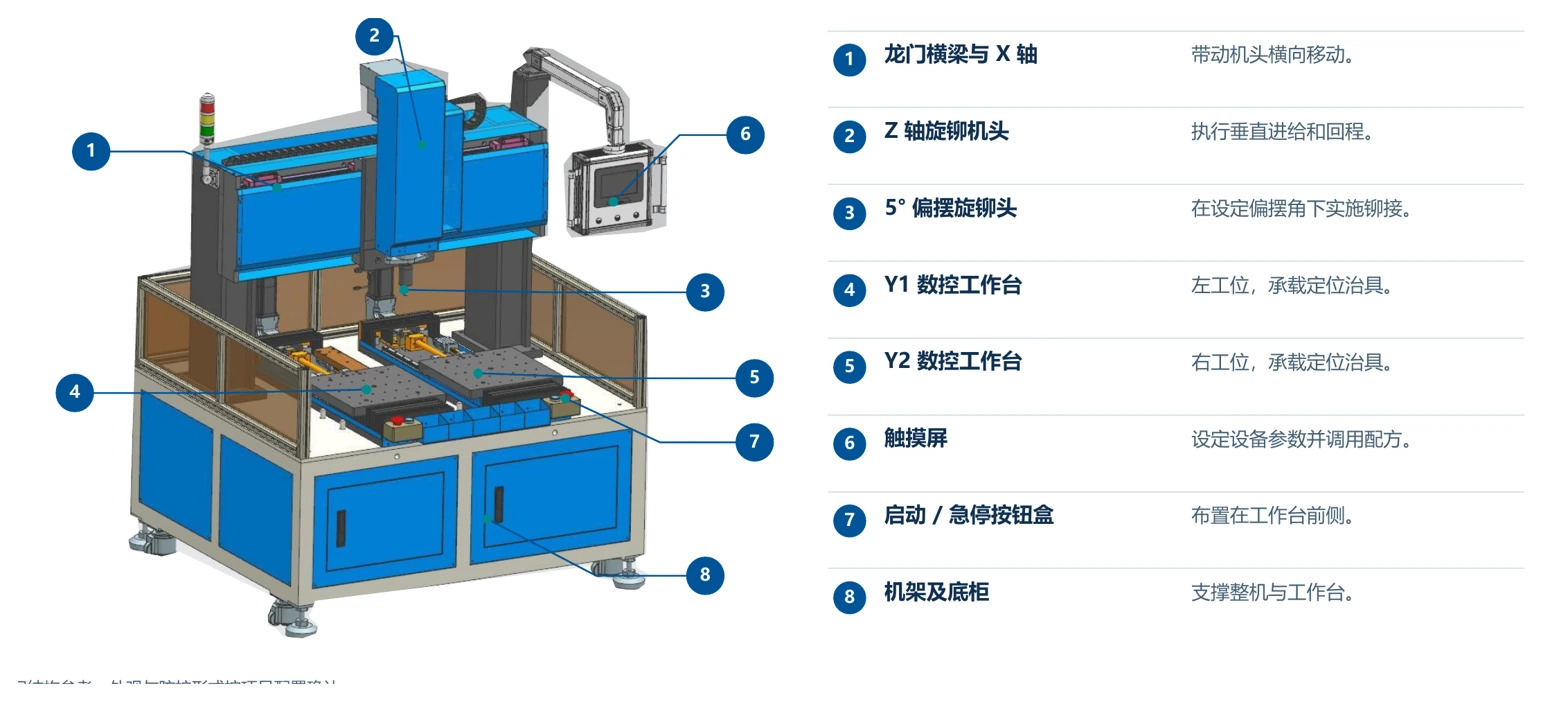
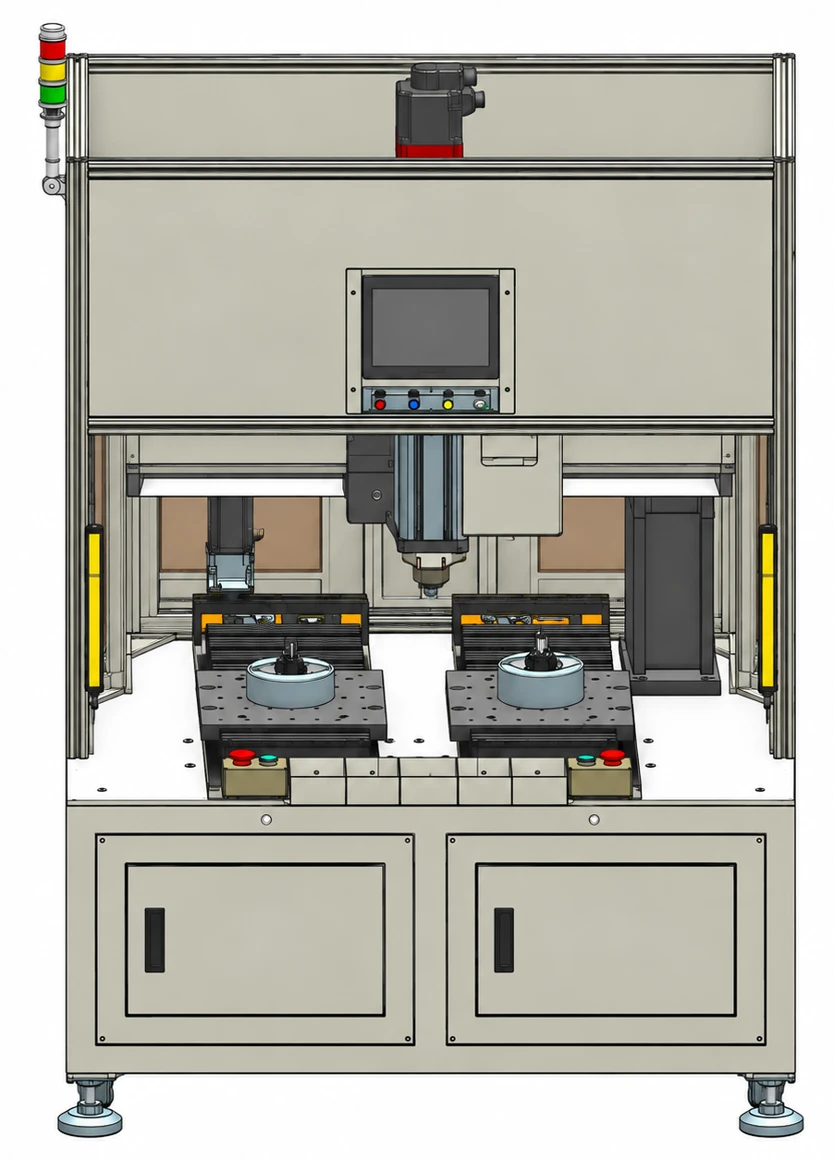
Two CNC worktables alternate positioning and riveting. Part loading at the other station depends on the agreed guarding and interlock design.
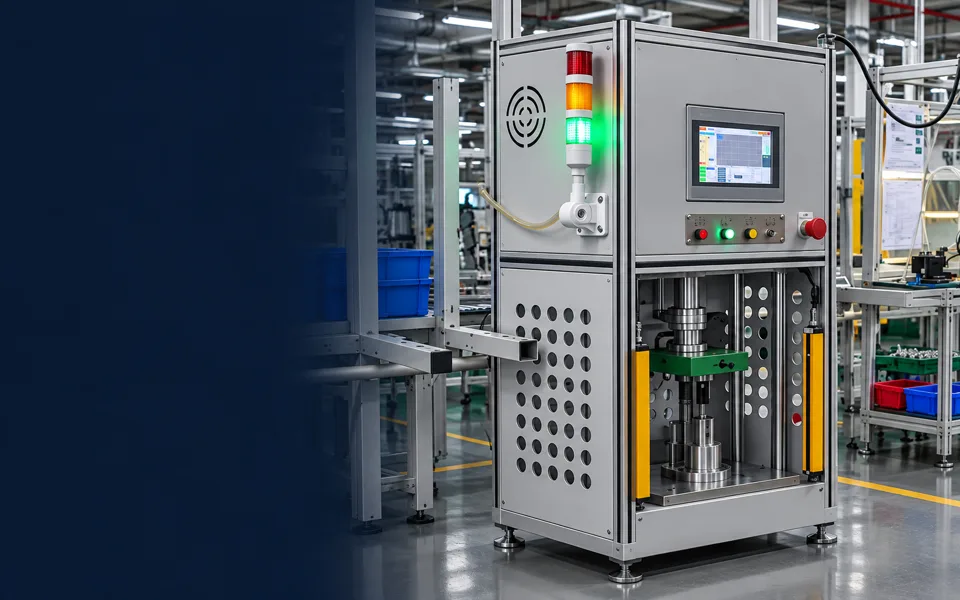
Engineering drawingsSee how the press station is loaded and operated on the factory floor. For your project, the force, tooling, and acceptance window are confirmed with representative samples.
Agree on parts, cycle time, and acceptance methods early, before tooling and station decisions become costly to revisit.
Review part geometry, fit tolerances, product mix, and loading method to define force, cycle time, and space constraints.
Use representative parts to confirm fixture support, final depth, and the force–displacement window.
Agree on guarding, data interfaces, fault handling, and the tests for factory and site acceptance.
Compare the frame, tooling envelope, and acceptance criteria after defining the part and cycle time. Final specifications are agreed for each project.
For front loading and changeovers. Reference stroke of 200 mm and a 350 × 290 mm worktable.
View C-frame configurationFor projects that need fixture support, guarding, and line integration. Reference stroke of 200 mm.
View four-column configurationBring part drawings, fit tolerances, fixture dimensions, a loading method, and target cycle time. Confirm working force and stroke with samples.
Define final depth and tolerance, pass and fault samples, a curve evaluation window, and the part IDs and results needed for traceability.
Agree what is included in the station and tooling, interface requirements, quotation assumptions, and factory and site acceptance criteria.
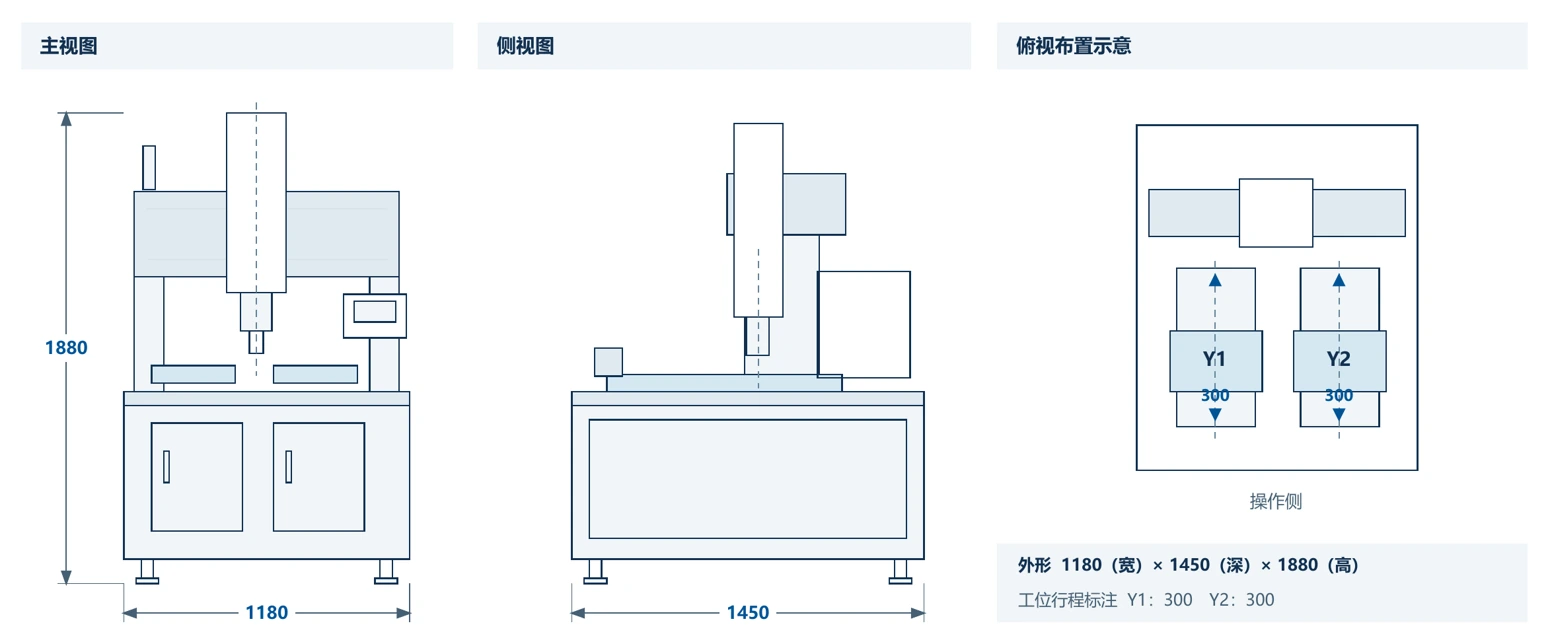
Review equipment components and site planning dimensions.
Use approved project drawings for fabrication and installation.
Based in Dongguan, Guangdong, we provide equipment selection and project engineering for servo pressing, riveting, and custom assembly workstations.
Send us your new line, capacity expansion, or retrofit requirements. Our engineering team can review the part and production conditions.
Attach shareable part drawings or photos to your email.